Soldering to Gold Over Nickel Surfaces
Total Page:16
File Type:pdf, Size:1020Kb
Load more
Recommended publications
-

Treatise on Combined Metalworking Techniques: Forged Elements and Chased Raised Shapes Bonnie Gallagher
Rochester Institute of Technology RIT Scholar Works Theses Thesis/Dissertation Collections 1972 Treatise on combined metalworking techniques: forged elements and chased raised shapes Bonnie Gallagher Follow this and additional works at: http://scholarworks.rit.edu/theses Recommended Citation Gallagher, Bonnie, "Treatise on combined metalworking techniques: forged elements and chased raised shapes" (1972). Thesis. Rochester Institute of Technology. Accessed from This Thesis is brought to you for free and open access by the Thesis/Dissertation Collections at RIT Scholar Works. It has been accepted for inclusion in Theses by an authorized administrator of RIT Scholar Works. For more information, please contact [email protected]. TREATISE ON COMBINED METALWORKING TECHNIQUES i FORGED ELEMENTS AND CHASED RAISED SHAPES TREATISE ON. COMBINED METALWORKING TECHNIQUES t FORGED ELEMENTS AND CHASED RAISED SHAPES BONNIE JEANNE GALLAGHER CANDIDATE FOR THE MASTER OF FINE ARTS IN THE COLLEGE OF FINE AND APPLIED ARTS OF THE ROCHESTER INSTITUTE OF TECHNOLOGY AUGUST ( 1972 ADVISOR: HANS CHRISTENSEN t " ^ <bV DEDICATION FORM MUST GIVE FORTH THE SPIRIT FORM IS THE MANNER IN WHICH THE SPIRIT IS EXPRESSED ELIEL SAARINAN IN MEMORY OF MY FATHER, WHO LONGED FOR HIS CHILDREN TO HAVE THE OPPORTUNITY TO HAVE THE EDUCATION HE NEVER HAD THE FORTUNE TO OBTAIN. vi PREFACE Although the processes of raising, forging, and chasing of metal have been covered in most technical books, to date there is no major source which deals with the functional and aesthetic requirements -
Scientific and Technical Report 2001 Volume VI Large Research Facilities
PAUL SCHERRER INSTITUT ISSN 1423-7350 March 2002 Scientific and Technical Report 2001 Volume VI Large Research Facilities ed. by: Renate Bercher, Carmen Büchli, Lotty Zumkeller CH-5232 Villigen PSI Switzerland Phone: 056/310 21 11 Telefax: 056/31021 99 http://www.psi.ch I TABLE OF CONTENTS Foreword l Accelerator Physics and Development Operation of the PSI-accelerator facility in 2001 5 Progress in the production of the new ring cyclotron cavity 7 Coupled field analysis of the new ring cyclotron cavity 9 Experimental upgrade of the injector II150 MHz RF system 11 Replacement of magnet power supplies, control and field-bus for the PSI cyclotron accelerators 13 Investigations on discharges of high voltage devices based on a transient recorder program 15 Test of a radio-frequency-driven mulitcusp proton source 16 Emittance measurements at the PSI ECR heavy ion source 17 Profile measurement of scanning proton beam for LiSoR using carbon fibre harps 18 A fast dégrader to set the energies for the application of the depth dose in proton therapy 20 MAD9P a parallel 3D particle tracker with space charge 22 Behaviour of the different poisson solvers in the light of beam dynamics simulations 24 Computational electrodynamics on the LINUX-cluster 26 Particle ray-tracing program TRACK applied to accelerators 27 Experimental Facilities Rebuilt beam line section between the targets M and E 31 Disposal preparation for meson production targets 33 A novel method to improve the safety of the planned MEGAPIE target at SINQ 34 Beamline adaptation for the MEGAPIE-target -

Sn95/Sb5 – Organic Acid 3% Core
Technical Data Sheet Sn95/Sb5 – Organic Acid 3% Core NOMINAL COMPOSITION Tin 94% Min Lead 0.1% Max Arsenic 0.01% Max Antimony 4.5% 5.5 Cadmium 0.005% Max Iron 0.04% Max Copper 0.08% Max Aluminum 0.005% Max Zinc 0.005% Max Silver 0.015% Max Bismuth 0.15% Max Flux – 3% Organic Acid Core by weight PHYSICAL PROPERTIES Solder Alloy Color White Melting Point (Solidus) 450°F (233°C) Flow Point (Liquidus) 464°F (240°C) Specific Gravity 7.26 Density (Lbs/in3) 0.263 Bulk Room Temperature Tensile Strength (PSI) 5,900 Flux Type Water Soluble Organic Acid Physical State Solid Melting Point 250°F (120°C) Chloride Content 4% SOLDERING CHARACTERISTICS Sn95/Sb5 is a general-purpose solder used in applications involving soldering of copper and copper alloys and/or ferrous base alloys where use of lead containing solder is not permitted. This soft solder may be used in applications involving higher service temperatures. Typical applications for this alloy include copper components in air conditioning industry. This alloy is also recommended in applications involving food handling or drinking water components where use of lead containing alloys is not permitted. Antimony bearing alloys are not recommended in soldering of brass parts due to formation of a brittle Sb-Zn inter-metallic. This flux-cored solder can be used on difficult to solder materials where rosin based fluxes and electronic grade organic fluxes are not strong enough. It has been used effectively in many non-electronic applications such as lamps, fuses, and jewelry. The flux is active on copper, brass, bronze, steel, nickel, and stainless steel. -
Low Melting Temperature Sn-Bi Solder
metals Review Low Melting Temperature Sn-Bi Solder: Effect of Alloying and Nanoparticle Addition on the Microstructural, Thermal, Interfacial Bonding, and Mechanical Characteristics Hyejun Kang, Sri Harini Rajendran and Jae Pil Jung * Department of Materials Science and Engineering, University of Seoul, 163, Seoulsiripdae-ro, Dongdaemun-gu, Seoul 02504, Korea; [email protected] (H.K.); [email protected] (S.H.R.) * Correspondence: [email protected] Abstract: Sn-based lead-free solders such as Sn-Ag-Cu, Sn-Cu, and Sn-Bi have been used extensively for a long time in the electronic packaging field. Recently, low-temperature Sn-Bi solder alloys attract much attention from industries for flexible printed circuit board (FPCB) applications. Low melting temperatures of Sn-Bi solders avoid warpage wherein printed circuit board and electronic parts deform or deviate from the initial state due to their thermal mismatch during soldering. However, the addition of alloying elements and nanoparticles Sn-Bi solders improves the melting temperature, wettability, microstructure, and mechanical properties. Improving the brittleness of the eutectic Sn-58wt%Bi solder alloy by grain refinement of the Bi-phase becomes a hot topic. In this paper, literature studies about melting temperature, microstructure, inter-metallic thickness, and mechanical properties of Sn-Bi solder alloys upon alloying and nanoparticle addition are reviewed. Keywords: low-temperature solder; Sn-58wt%Bi; melting temperature; microstructure; mechani- Citation: Kang, H.; Rajendran, S.H.; cal property Jung, J.P. Low Melting Temperature Sn-Bi Solder: Effect of Alloying and Nanoparticle Addition on the Microstructural, Thermal, Interfacial Bonding, and Mechanical 1. Introduction Characteristics. Metals 2021, 11, 364. -
The Development of the Periodic Table and Its Consequences Citation: J
Firenze University Press www.fupress.com/substantia The Development of the Periodic Table and its Consequences Citation: J. Emsley (2019) The Devel- opment of the Periodic Table and its Consequences. Substantia 3(2) Suppl. 5: 15-27. doi: 10.13128/Substantia-297 John Emsley Copyright: © 2019 J. Emsley. This is Alameda Lodge, 23a Alameda Road, Ampthill, MK45 2LA, UK an open access, peer-reviewed article E-mail: [email protected] published by Firenze University Press (http://www.fupress.com/substantia) and distributed under the terms of the Abstract. Chemistry is fortunate among the sciences in having an icon that is instant- Creative Commons Attribution License, ly recognisable around the world: the periodic table. The United Nations has deemed which permits unrestricted use, distri- 2019 to be the International Year of the Periodic Table, in commemoration of the 150th bution, and reproduction in any medi- anniversary of the first paper in which it appeared. That had been written by a Russian um, provided the original author and chemist, Dmitri Mendeleev, and was published in May 1869. Since then, there have source are credited. been many versions of the table, but one format has come to be the most widely used Data Availability Statement: All rel- and is to be seen everywhere. The route to this preferred form of the table makes an evant data are within the paper and its interesting story. Supporting Information files. Keywords. Periodic table, Mendeleev, Newlands, Deming, Seaborg. Competing Interests: The Author(s) declare(s) no conflict of interest. INTRODUCTION There are hundreds of periodic tables but the one that is widely repro- duced has the approval of the International Union of Pure and Applied Chemistry (IUPAC) and is shown in Fig.1. -
Major Causes of Solder Cracks Applications and Boards That Specially Require Solder Crack Countermeasures Comparison of 2 Soluti
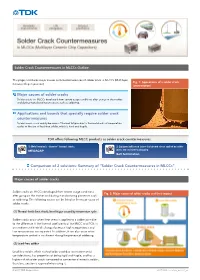
Solder Crack Countermeasures in MLCCs Outline This page introduces major causes and countermeasures of solder crack in MLCCs (Multilayer Fig. 1: Appearance of a solder crack Ceramic Chip Capacitors). (cross-section) Major causes of solder cracks Solder cracks on MLCCs developed from severe usage conditions after going on the market and during manufacturing processes such as soldering. Applications and boards that specially require solder crack countermeasures Solder cracks occur mainly because of thermal fatigue due to thermal shock or temperature cycles or the use of lead-free solder, which is hard and fragile. TDK offers following MLCC products as solder crack countermeasures. 1) Metal terminals “disperse” thermal shock : 2) Equipped with resin layers that absorb stress applied on solder MEGACAP joints and resistant to dropping: Soft termination Comparison of 2 solutions: Summary of “Solder Crack Countermeasures in MLCCs” Major causes of solder cracks Solder cracks on MLCCs developed from severe usage conditions Fig. 2: Major causes of solder cracks and their impact after going on the market and during manufacturing processes such as soldering. The following causes can be listed as the major cause of solder cracks. (1) Thermal shock (heat shock), heat fatigue caused by temperature cycle Solder cracks occur when heat stress is applied to a solder joint due to the difference in the thermal coefficients of the MLCC and PCB, in an environment in which changes between high temperatures and low temperatures are repeated. In addition, it can also occur when temperature control is insufficient during the process of soldering. (2) Lead-free solder Lead-free solder, which started to be used due to environmental considerations, has properties of being rigid and fragile, and has a higher risk of solder cracks compared to conventional eutectic solder; therefore, caution is required when using it. -
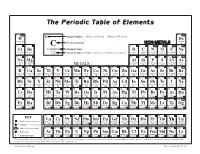
The Periodic Table of Elements
The Periodic Table of Elements 1 2 6 Atomic Number = Number of Protons = Number of Electrons HYDROGENH HELIUMHe 1 Chemical Symbol NON-METALS 4 3 4 C 5 6 7 8 9 10 Li Be CARBON Chemical Name B C N O F Ne LITHIUM BERYLLIUM = Number of Protons + Number of Neutrons* BORON CARBON NITROGEN OXYGEN FLUORINE NEON 7 9 12 Atomic Weight 11 12 14 16 19 20 11 12 13 14 15 16 17 18 SODIUMNa MAGNESIUMMg ALUMINUMAl SILICONSi PHOSPHORUSP SULFURS CHLORINECl ARGONAr 23 24 METALS 27 28 31 32 35 40 19 20 21 22 23 24 25 26 27 28 29 30 31 32 33 34 35 36 POTASSIUMK CALCIUMCa SCANDIUMSc TITANIUMTi VANADIUMV CHROMIUMCr MANGANESEMn FeIRON COBALTCo NICKELNi CuCOPPER ZnZINC GALLIUMGa GERMANIUMGe ARSENICAs SELENIUMSe BROMINEBr KRYPTONKr 39 40 45 48 51 52 55 56 59 59 64 65 70 73 75 79 80 84 37 38 39 40 41 42 43 44 45 46 47 48 49 50 51 52 53 54 RUBIDIUMRb STRONTIUMSr YTTRIUMY ZIRCONIUMZr NIOBIUMNb MOLYBDENUMMo TECHNETIUMTc RUTHENIUMRu RHODIUMRh PALLADIUMPd AgSILVER CADMIUMCd INDIUMIn SnTIN ANTIMONYSb TELLURIUMTe IODINEI XeXENON 85 88 89 91 93 96 98 101 103 106 108 112 115 119 122 128 127 131 55 56 72 73 74 75 76 77 78 79 80 81 82 83 84 85 86 CESIUMCs BARIUMBa HAFNIUMHf TANTALUMTa TUNGSTENW RHENIUMRe OSMIUMOs IRIDIUMIr PLATINUMPt AuGOLD MERCURYHg THALLIUMTl PbLEAD BISMUTHBi POLONIUMPo ASTATINEAt RnRADON 133 137 178 181 184 186 190 192 195 197 201 204 207 209 209 210 222 87 88 104 105 106 107 108 109 110 111 112 113 114 115 116 117 118 FRANCIUMFr RADIUMRa RUTHERFORDIUMRf DUBNIUMDb SEABORGIUMSg BOHRIUMBh HASSIUMHs MEITNERIUMMt DARMSTADTIUMDs ROENTGENIUMRg COPERNICIUMCn NIHONIUMNh -

Galvalume Facts
GALVALUME FACTS Soldering Although GALVALUME® steel sheet can be soldered, the presence of a thin film of aluminum oxide on the surface makes soldering more difficult than when soldering galvanized products. When soldering is necessary, the techniques and fluxes used to solder aluminum should be used. Welding GALVALUME® steel sheet can be welded by conventional resistance and arc welding processes. The safety precautions are similar to those for hot-dip galvanized sheet. Because the surface contact resistance is low when compared with uncoated sheet, resistance welding of GALVALUME® steel sheet requires welding currents, welding times and electrode forces higher than those required for similar thicknesses of uncoated cold rolled steel. These welding parameters are similar to those normally used on galvanized steel. However, experience has shown that even more frequent electrode dressing is required, as compared with galvanized sheet, to achieve good welds. There is less fuming when welding GALVALUME® steel sheet than when welding galvanized sheet. The coating contains less zinc than a comparably thick galvanized coating. Nevertheless, adequate ventilation is required to remove the zinc oxide fumes. Fastening From a mechanical standpoint, any style of fastener suitable for use with sheet metal can be used to join GALVALUME® steel sheet to itself or to other parts, provided the fastener design is appropriate for the structural requirement of the application. The list of acceptable devices includes common fasteners like nuts and bolts, screws and rivets of all types, and special types like clamp fasteners, clips and blind screws. Corrosion characteristics of the fastener material should be carefully considered from two standpoints. -
Procedure 4.0—Hot Work Program (Hwp)
Hamilton College Occupational Health and Safety Procedures PROCEDURE 4.0—HOT WORK PROGRAM (HWP) 4.1 INTRODUCTION Purpose Regulations promulgated by the Occupational Safety and Health Administration (OSHA—29 CFR 1910.252— Welding, Cutting and Brazing) and the NYS Fire Code (Code Chapter 26—Hot Work) require facilities to develop procedures to protect both human health and welfare, and the facility itself, from the hazards posed by hot work in the workplace. This program is intended to provide the Hamilton College community with the guidance necessary to comply with these regulations. Scope Hamilton College is committed to providing a safe and healthful work environment for its students, employees and the greater college community. The following Hot Work Program (HWP) has been developed to eliminate or minimize risks to personnel, students, and campus facilities. While the greatest hot work risks arise from spark/slag producing activity (welding, cutting, brazing), other forms of hot work (pipe soldering, pipe thawing, etc.) may also present risks in the form of radiant heat and/or open flame. As such, certain elements of this program will pertain to all types of hot work activity, and others will only address the more dangerous activities that produce sparks. This HWP includes: • Identification of Responsibilities • Prohibited Hot Work Areas/Activities • Welding/Cutting/Brazing Authorization Process • Hot Work Permits • Special Considerations for Soldering/Other Hot Work Activities • Fire Watch • Contractors Applicability The Director of Environmental Protection, Safety & Sustainability (EPS&S) will maintain and update the College’s written Hot Work Program, and will work primarily with other relevant parties (the Physical Plant and certain academic departments) for training and compliance purposes. -

Soldering to Gold Films
Soldering to Gold Films THE IMPORTANCE OF LEAD-INDIUM ALLOYS Frederick G. Yost Sandia Laboratories, Albuquerque, New Mexico, U.S.A. Reliable solder joints can be made on gold metallised microcircuits using lead-indium solders providing certain important conditions are understood and carefully controlled. This paper reviews the three fundamental concepts of scavenging, wetting, and ageing, which are relevant when soldering to gold films. Alloys containing indium have been used for solder- sition and a body centred tetragonal space lattice. ing electronic components to thin gold films and wires Although considerable work has been addressed for at least 14 years. Braun (1, 2) investigated the to the question of clustering and phase separation potential of several multicomponent alloys based in the a field below 20°C (7, 8, 9) the practical signifi- upon the lead-tin-indium ternary alloy system. cance of this phenomenon has not yet materialised. More recently, work on lead-indium binary alloys The most commonly used alloy is the 50 weight has been reported by Jackson (3) and Yost, et al per cent indium composition which has a liquidus (4, 5, 6). In this paper we intend to define, to discuss, temperature of approximately 210°C and a solidus and to illustrate three fundamental concepts relevant temperature of approximately 185°C. Alloys in the to soldering to gold films using lead-indium solders. lead rich phase field, a, freeze dendritically by The lead-indium phase diagram, shown in Figure forming lead rich stalks. The formation of these 1, contains a wealth of useful solder alloys having dendrites causes a surface rumpling which gives the solidus temperatures which range from 156.6°C solder surface a somewhat frosty rather than a shiny (pure indium) to 327.5 °C (pure lead). -

Footnotes for ATOMIC ADVENTURES
Footnotes for ATOMIC ADVENTURES Secret Islands, Forgotten N-Rays, and Isotopic Murder - A Journey into the Wild World of Nuclear Science By James Mahaffey While writing ATOMIC ADVENTURES, I tried to be careful not to venture off into subplots, however interesting they seemed to me, and keep the story flowing and progressing at the right tempo. Some subjects were too fascinating to leave alone, and there were bits of further information that I just could not abandon. The result is many footnotes at the bottom of pages, available to the reader to absorb at his or her discretion. To get the full load of information from this book, one needs to read the footnotes. Some may seem trivia, but some are clarifying and instructive. This scheme works adequately for a printed book, but not so well with an otherwise expertly read audio version. Some footnotes are short enough to be inserted into the audio stream, but some are a rambling half page of dense information. I was very pleased when Blackstone Audio agreed wholeheartedly that we needed to include all of my footnotes in this version of ATOMIC ADVENTURES, and we came up with this added feature: All 231 footnotes in this included text, plus all the photos and explanatory diagrams that were included in the text. I hope you enjoy reading some footnotes while listening to Keith Sellon-Wright tell the stories in ATOMIC ADVENTURES. James Mahaffey April 2017 2 Author’s Note Stories Told at Night around the Glow of the Reactor Always striving to beat the Atlanta Theater over on Edgewood Avenue, the Forsyth Theater was pleased to snag a one-week engagement of the world famous Harry Houdini, extraordinary magician and escape artist, starting April 19, 1915.1 It was issued an operating license, no. -

Photochemical Machining
Design Guide to Photochemical Machining A World Apart in a World of Parts This “Design Guide to Photochemical Machining” was cre- ated for those involved with the designing or purchasing of Fotofab uses a special process called Photochemical Machining. Also known as chemical etching, acid etching, or milling, this process metal parts. While it provides general guidelines, Fotofab’s offers many advantages over traditional metal fabrication methods: Technical Sales Staff is available to assist Speed you with your specifi c requirements. • Tooling can be produced rapidly. • Parts can be produced and shipped within hours of receiving a print. By designing with an awareness of our process capabilities, you will minimize Flexibility • Many intricate part geometries, like those found in fi ne resolution the cost and delivery time of your metal screens, can be photochemically machined easily and economically. parts. We are ready to work with you, • Revisions to part designs are implemented quickly and inexpensively. • Brittle metals, which often fracture during conventional stamping, are machined without diffi culty. Just tell us what you need! Repeatability • Prototype and production quantities can be made using the same process and tooling. Contents • Extremely thin metal can be machined without distortion; dimensional accuracy actually increases as metal thickness decreases. The Fotofab Process • page 4 • Physical properties of the metal, such as hardness, strength and formability, are not changed by the process. Value-Added Services • page 7 • Magnetically soft materials can be fabricated while retaining their optimum permeability. Applications • page 8 • Parts are inherently free of burrs. Material Selection • page 10 Cost Effectiveness • Tooling and set-up costs are extremely low compared to hard tooling.